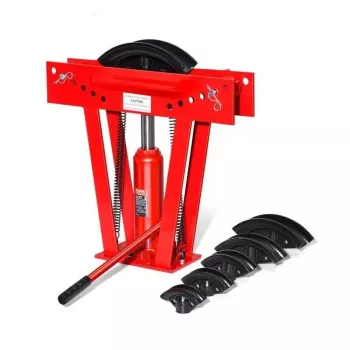
A hydraulic pipe bender is a practical upgrade when hand benders start kinking tubing or demand more muscle than the job should require. This 12-ton bender uses a bottle-jack style hydraulic ram to apply steady, controllable pressure—helping produce smoother bends for shop projects like exhaust routing, handrails, trailer work, and general fabrication. With six included dies, it’s designed for repeatable bends across common pipe sizes while keeping setup straightforward for home garages and small workshops.
If you’re building out a capable DIY metalworking setup, pair it with a solid forming surface like the Single Horn Cast Steel Anvil with Round Horn and Stable Base for Metal Work for straightening, shaping, and general fit-up tasks.
A press-style hydraulic bender is meant to take the struggle out of bending and make outcomes more consistent from piece to piece—especially when you’re doing more than one bend or trying to match a prior part.
For the current in-stock unit, see 12 Ton Hydraulic Pipe Bender with 6 Dies for Copper, Steel & Exhaust Tubing.
This style of bender relies on controlled hydraulic force rather than a long handle and a fast pull. That controlled pace is what makes it easier to “sneak up” on an angle and keep bends consistent.
| Stage | What to do | Why it matters |
|---|---|---|
| 1. Measure & mark | Mark bend start, direction, and target angle | Improves repeatability and reduces rework |
| 2. Select die | Choose the die that matches the pipe size | Incorrect dies increase kinks/flattening |
| 3. Align in frame | Seat pipe squarely and center the mark | Prevents twisting and uneven bends |
| 4. Bend gradually | Pump to advance, pause to check angle | Avoids overshooting the target |
| 5. Release pressure | Back off pressure slowly and remove pipe | Helps maintain shape and reduces springback surprises |
The six-die set is what makes this tool practical for a wide range of shop tasks, but bend quality hinges on choosing the closest match and setting expectations based on the material you’re bending.
General guarding and safe-operation principles for shop equipment are outlined by OSHA’s machine guarding guidance. While a pipe bender isn’t a production press brake, the same mindset applies: keep your body out of pinch zones, maintain stable footing, and don’t reach into the working area while the tool is loaded.
Copper can bend cleanly, but it also shows marks easily. Keep dies and tube surfaces clean and move slowly so the tube stays seated as the bend develops. If you’re working with copper tube used in plumbing or HVAC contexts, review handling and material notes from the Copper Development Association copper tube handbook.
| Item | Detail |
|---|---|
| Product | 12 Ton Hydraulic Pipe Bender with 6 Dies for Copper, Steel & Exhaust Tubing |
| Price | 221.51 USD |
| Availability | In stock |
| Included | Six dies (set) |
When you’re ready to outfit your workspace, the 12 Ton Hydraulic Pipe Bender with 6 Dies for Copper, Steel & Exhaust Tubing is a strong foundation for bending tasks, and the Single Horn Cast Steel Anvil complements it for shaping and finishing.
It can, but results depend heavily on tubing wall thickness, how closely the die matches the tube’s outside diameter, and the bend radius being formed. Bend gradually, check alignment often, and test on scrap—very thin-wall exhaust tubing can still deform with press-style benders.
The die should match the pipe or tube outside diameter so the material is supported through the bend. A die that’s too large reduces support and increases flattening or kinking; a die that’s too small may mar the surface, pinch the tube, or prevent proper seating.
Springback varies by alloy and wall thickness, but steel typically rebounds more than copper. Pump in small increments, check the angle frequently, and plan for a slight overbend to land on your final angle after release.


Leave a comment